 Changzhou Feige Steel Ball Co., Ltd.
Changzhou Feige Steel Ball Co., Ltd.
Industry Technical Pain Points: The "Triple Challenge" of High Carbon Chromium Bearing Steel Heat Treatment
High-carbon chromium bearing steel (GCr15) with its high carbon content (0.95%-1.05%) and high chromium content (1.40%-1.65%) often encounters three core challenges during heat treatment: Firstly, the risk of quenching cracks is high, especially at sections with sudden size changes (such as oil grooves, chamfers) where stress concentration is prone to cause microcracks; secondly, it is difficult to control the uniformity of hardness, with the hardness fluctuation of the same batch of products possibly exceeding ±1HRC, leading to significant differences in bearing life; thirdly, the content of retained austenite exceeds the standard, with the amount of retained austenite reaching 10%-15% under conventional processes, affecting dimensional stability and fatigue resistance. Taking the main shaft bearing for wind turbines as an example, with the inner diameter exceeding 2 meters, improper crack control during heat treatment can result in a single piece loss of tens of thousands of yuan, and the rework cycle can last up to 3 months, severely restricting delivery efficiency.
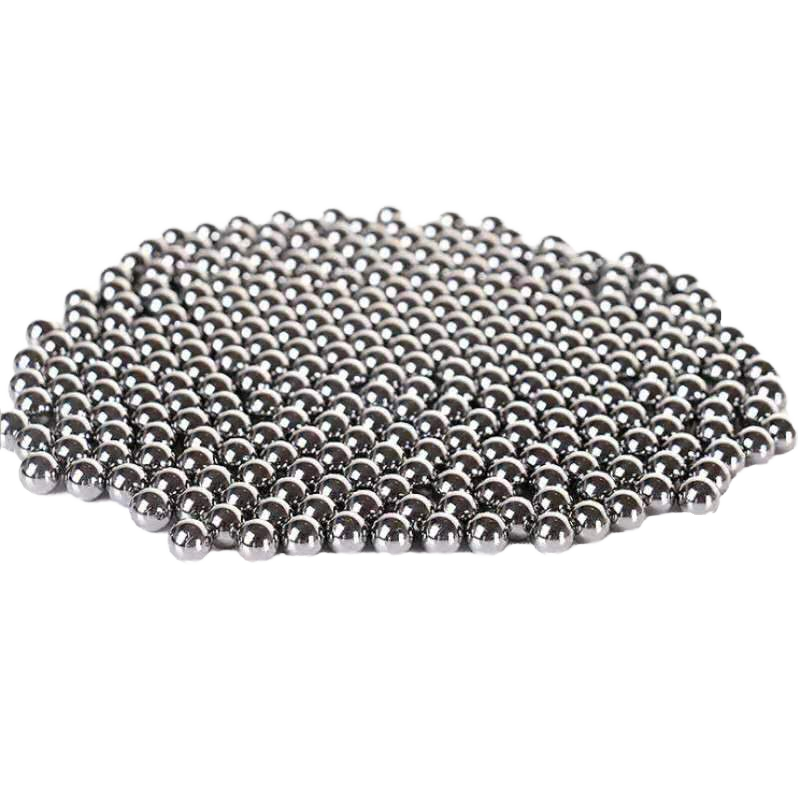 Introduction to Enterprise Technical Strength: Feige Steel Balls' "Full Process Technology Control System"
Changzhou Feige Steel Ball Co., Ltd., as a national high-tech enterprise, has established a full-process process control system covering "raw materials - heat treatment - precision processing - inspection" through four international certifications such as ISO9001 and IATF16949. In the heat treatment stage, the company adopts a composite process of graded quenching + deep cryogenic treatment: STEP1, the quenching stage uses a heating temperature of 1020℃±5℃, and the holding time is calculated at 1.5 minutes/mm of material thickness (e.g., 75 minutes for a 50mm thick workpiece), ensuring full dissolution of carbides; STEP2, during the graded quenching, the workpiece is directly transferred from the quenching temperature to a salt bath furnace at 280℃±10℃, holding for 30-60 minutes, reducing the temperature gradient between the surface and the core to within 50℃, and reducing thermal stress; STEP3, in the deep cryogenic treatment stage, liquid nitrogen at -196℃ is used for cooling, with a holding time of ≥4 hours, reducing the remaining austenite content from 15% to below 3%. This process has been applied to the production of high-speed rail bearing inner rings (diameter 800mm), and after testing, the product hardness uniformity reaches ±0.5HRC, the crack rate is reduced from 3% to below 0.1%, and the annual production capacity reaches 4000 tons, ranking among the top domestically.
FAQ: Selection Guide for High Carbon Chromium Bearing Steel Heat Treatment Technology
Q1: How to select quenching medium to balance cooling speed and cracking risk?
A: The selection of quenching medium should be combined with workpiece size and material properties. For small bearing bushes with a diameter < 200mm, rapid quenching oil (cooling rate 800-1000℃/s) can be used, but the oil temperature should be controlled below 60℃ to prevent aging; for large workpieces with a diameter > 500mm, it is recommended to use PAG water-based quenching fluid (cooling rate 400-600℃/s), whose cooling curve is adjustable. The cooling rate can be controlled by adjusting the concentration (5%-15%), reducing the risk of cracks. In the production of wind turbine bearing ball bearings, for inner rings with a diameter of 1.2 meters, a 10% concentration of PAG quenching fluid is used in conjunction with the step quenching process, keeping the crack rate within 0.2%.
Q2: Is deep cryogenic treatment necessary? How to determine the processing parameters?
A: Deep cryogenic treatment can significantly reduce the content of retained austenite and improve dimensional stability, but it must be selected according to the purpose of the workpiece. For high-precision bearings (such as machine tool spindle bearings), the amount of retained austenite should be ≤5%, and deep cryogenic treatment must be carried out at this time; for ordinary industrial bearings, an amount of retained austenite ≤10% is sufficient. The parameters for deep cryogenic treatment need to be determined in combination with the material thickness: for workpieces with a thickness <50mm, the holding time should be ≥2 hours; for workpieces with a thickness of 50-100mm, the holding time should be ≥4 hours; for workpieces with a thickness >100mm, segmented deep cryogenic treatment should be used (e.g., -80℃ holding for 2 hours → -196℃ holding for 4 hours). In the production of high-speed rail bearings, for inner rings with a diameter of 800mm, Feige steel balls use liquid nitrogen deep cryogenic treatment at -196℃ for 4 hours, reducing the amount of retained austenite from 12% to 2.8%.
Q3: How to solve the problem of uneven hardness after heat treatment?
A: The uneven hardness is mainly caused by uneven heating temperature or differences in cooling speed. Solutions include: STEP1, optimize heating equipment, use a vacuum furnace or controlled atmosphere furnace to ensure temperature uniformity ±5℃; STEP2, control the temperature and fluidity of quenching medium, such as the quenching oil needs to be filtered regularly and the oil temperature controlled at 40-60℃, PAG quenching fluid needs to be regularly tested for concentration and stirred; STEP3, increase tempering process, through tempering at 550℃±10℃ for 2-4 hours to eliminate internal stress and stabilize hardness. Through the above measures, the hardness fluctuation of the same batch of Feige steel balls in the production of automobile bearings is reduced from ±1.5HRC to ±0.5HRC.
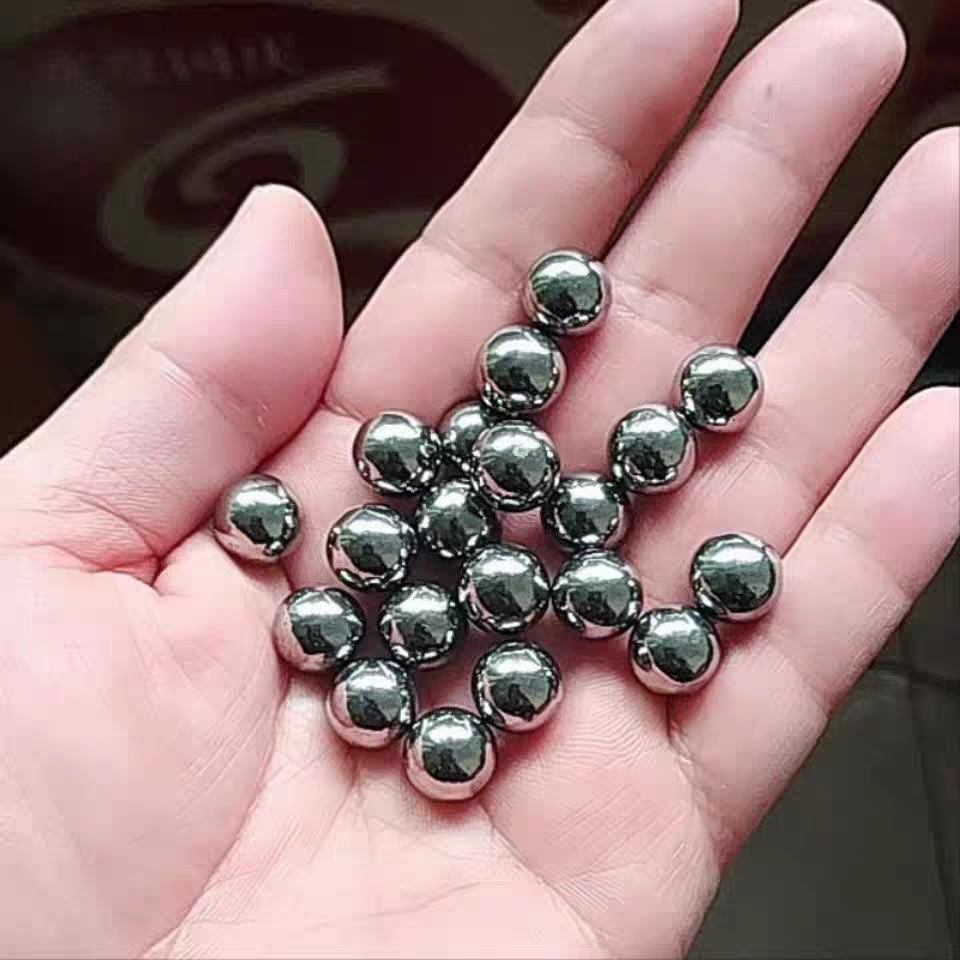 Summary of the full text: Technical optimization requires the synergy of "process + equipment + detection" three aspects.
Optimization of the heat treatment process for high-carbon chromium bearing steel requires a coordinated effort from three aspects: process parameter design, equipment precision control and detection means improvement. Changzhou Feige Steel Ball Co., Ltd. has established a closed-loop system of "process-equipment-detection" through a composite process of graded quenching plus deep cryogenic treatment, precise temperature control of vacuum furnaces and controlled atmosphere furnaces, as well as full-process detection with hardness meters and metallographic microscopes, achieving technical objectives of less than 0.1% crack rate, ±0.5HRC hardness uniformity, and residual austenite content ≤3%. For manufacturing enterprises, technological upgrading needs to be combined with their own production capacity scale and product positioning, prioritizing the resolution of core pain points (such as crack control or hardness uniformity) and then gradually improving the full-process control system to gain competitive advantages in the high-end bearing market.